Austenitising and Homogenisation
Explore the role of heating in austenitising and homogenisation, considering material structure, temperature distribution and holding time together.
The process
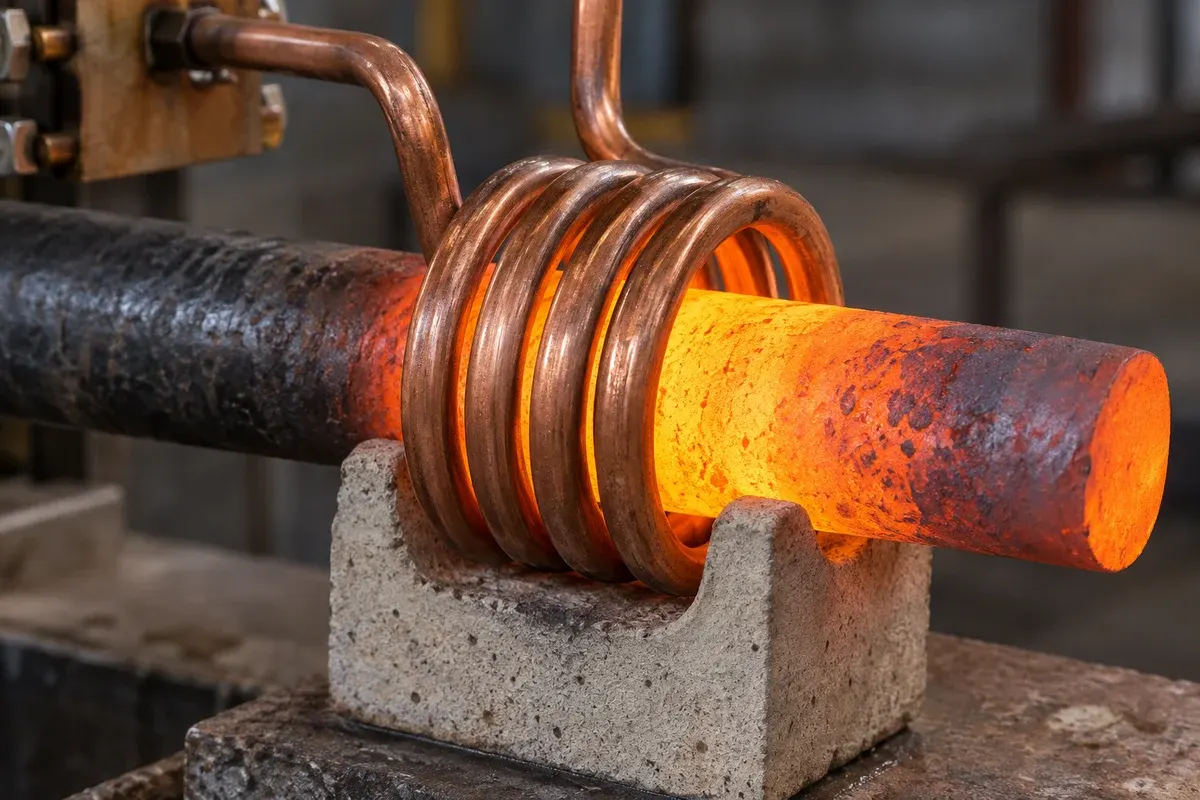
Austenitising brings suitable steels into the austenitic region during heat treatment. Homogenisation is a separate treatment determined by the material and the intended outcome; the two processes do not use the same treatment cycle.
Where it is used
The suitability of induction depends on the alloy, cross-section, required temperature distribution and holding time. The heating method alone does not guarantee the intended metallurgical result.
Key considerations
- Alloy and initial material structure
- Required heat treatment and holding time
- Temperature distribution through the cross-section and method of verification
Explore other applications
Billet Heating
Explore induction heating for billets before forging and forming, including the effects of material, cross-section and production flow on the process.
Read more ↗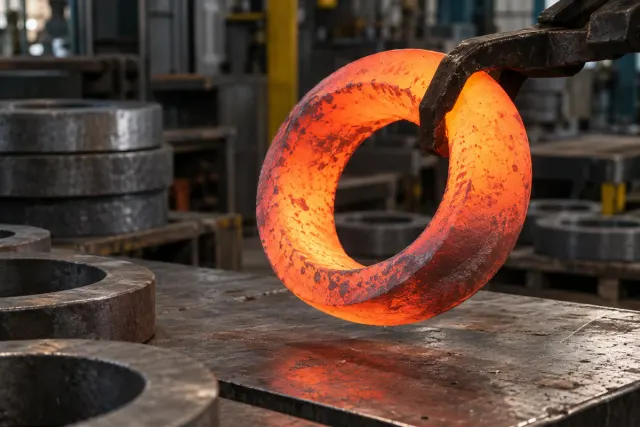
Preheating for Ring Rolling
Learn how ring blanks are heated before rolling and how material, cross-section and temperature distribution affect preparation for the forming process.
Read more ↗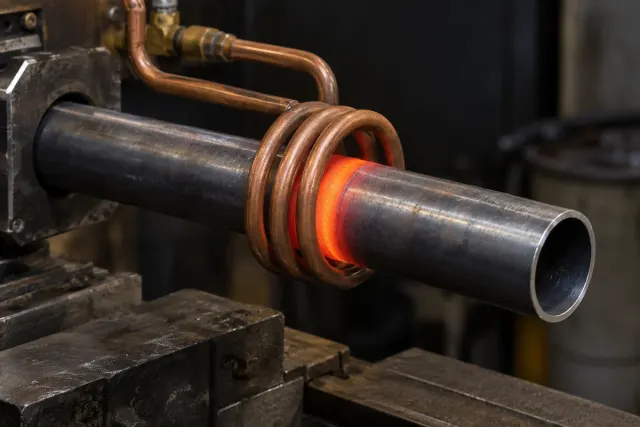
Bar and Tube Heating
Explore localised and full-length induction heating for bars and tubes, with process selection based on component geometry, diameter and wall thickness.
Read more ↗Ingot Heating for Forging
Understand ingot heating before forging, from material selection and temperature distribution to transfer arrangements for the press or hammer.
Read more ↗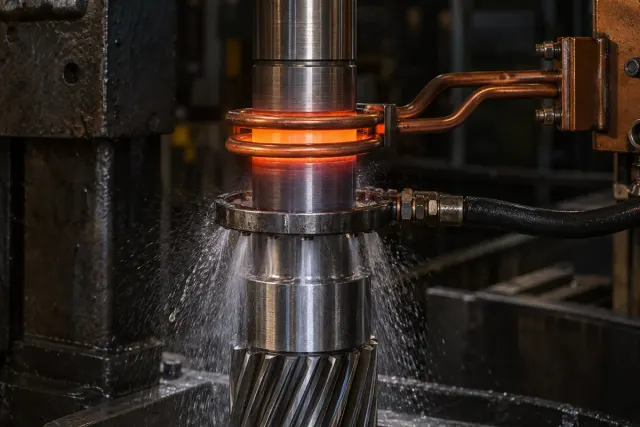
Heat Treatment
Learn how induction heat treatment affects material properties and why local heating, cooling conditions and process verification must be assessed together.
Read more ↗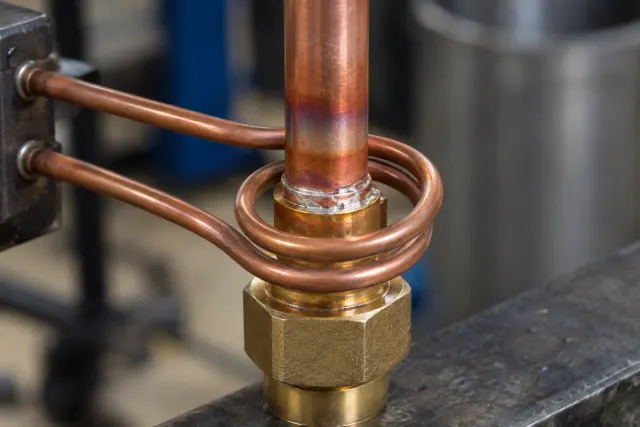
Brazing and Welding
Understand induction heating in metal joining, including the differences between brazing and welding and the role of joint geometry and material selection.
Read more ↗
Shrink Fitting
Explore controlled heating for interference-fit assembly, including thermal expansion, fit tolerances and the temperature limits of individual components.
Read more ↗Surface Treatment
Discover the principles of induction surface hardening and how material selection, the heated area and cooling conditions determine surface properties.
Read more ↗Get a quote for your project
Tell us about your application; our engineers will reply within 24 hours.
How does locally manufactured equipment compare with imported systems?
For buyers in Türkiye, imported systems can involve exchange-rate exposure, longer delivery times, expensive spare parts and dependence on overseas service. Local manufacture can offer faster service and coil production, on-site commissioning, operator training, payment in Turkish lira and competitive investment costs. More automotive suppliers and foundries are bringing induction hardening and melting in-house; energy savings and increased capacity can contribute to the return on investment. Compare the quality of power electronics, IGBT inverters, PLC controls, protection functions and reference installations when making a decision.
How do induction furnaces compare with gas-fired and electric arc furnaces?
Induction furnaces convert approximately 60–85% of electrical energy into useful heat, reaching up to 90% in some systems, compared with typical figures of 35–55% for combustion-based furnaces. Compared with a cupola furnace, induction offers closer control of melt composition and temperature, lower gas and slag content, and improved working conditions without on-site combustion. The main trade-offs are higher initial investment and dependence on electricity prices. A comparison should consider total cost of ownership, including energy, refractories, maintenance and labour.
Which processes use induction heating equipment?
Industrial induction equipment is used throughout metal processing: melting in foundries; surface hardening of shafts, gears, crankshafts and camshafts; preheating for forging; brazing; annealing and tempering; stress relieving; shrink-fit assembly and disassembly; pipe bending; and pre- and post-weld heat treatment. Maintenance applications include releasing seized bolts. Major users include the automotive, foundry, aerospace, defence, energy, tooling and machinery industries.
Is induction heating safe, and what about magnetic-field exposure?
Induction heating uses no open flame, flammable gas or combustion products, removing several hazards associated with conventional furnaces. The electromagnetic field is non-ionising and must be assessed against applicable exposure requirements, including standards such as IEEE C95.1 and C95.6. Personnel with active medical implants, such as pacemakers, should not work close to the coil; magnetic cards and sensitive electronics should remain outside the field. High temperatures and molten metal remain significant hazards, requiring appropriate heat-treatment protective equipment and operating procedures.
What maintenance does an induction system need, and how long can it operate?
Contact-free heating and the absence of moving parts in the heating unit keep mechanical wear low. Modern solid-state inverter systems are designed for long service. Key maintenance tasks include monitoring cooling-water quality and flow, controlling scale and corrosion, checking coil insulation, inspecting and tightening electrical connections, and calibrating pyrometers or thermocouples. Protection against overcurrent, overvoltage, phase faults, water interruption and excessive temperature, together with alarm-history review, supports condition-based maintenance.